Capabilities / Manufacturing
Three facilities.
Three distinct strengths.
One Symbio standard.
Each facility has a clear job to do. Together, they give Symbio focused manufacturing capability across APIs, pharmaceutical enzymes and value-added pre-formulations.
Flagship API manufacturing
Vizag Facility
Flagship API manufacturing for regulated-market growth.
150 KL
Operational capacity
+200 KL
Capacity expansion underway
Up to ~600 KL
Long-term site capacity potential
The ~600 KL figure is long-term site capacity potential, not current commissioned capacity.
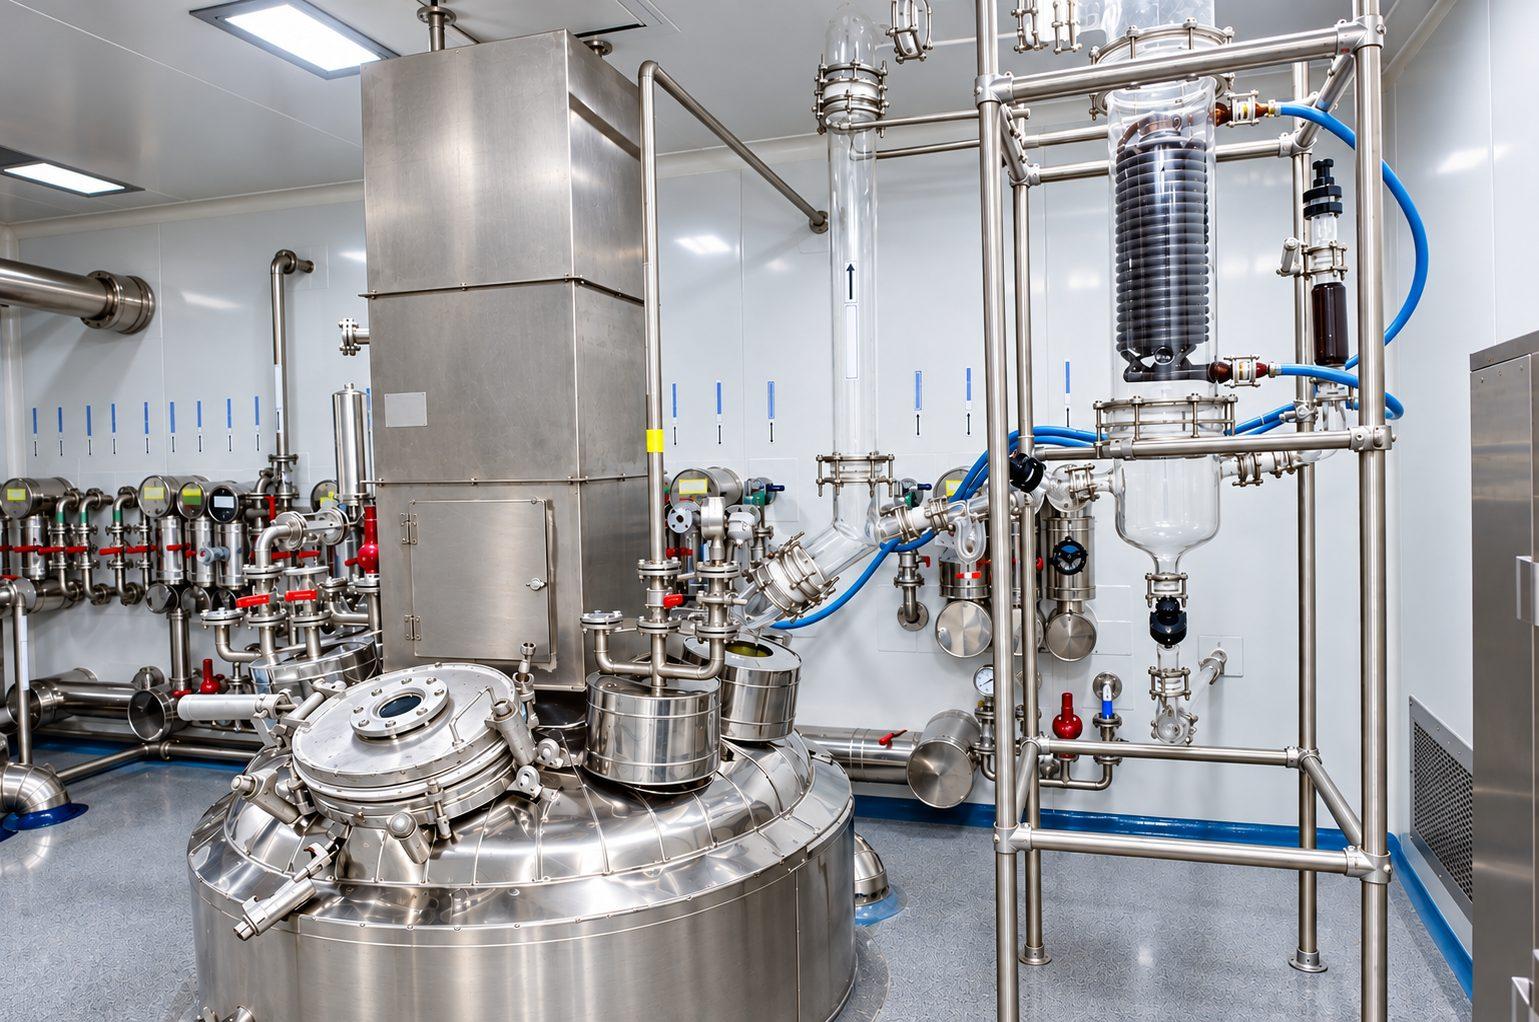
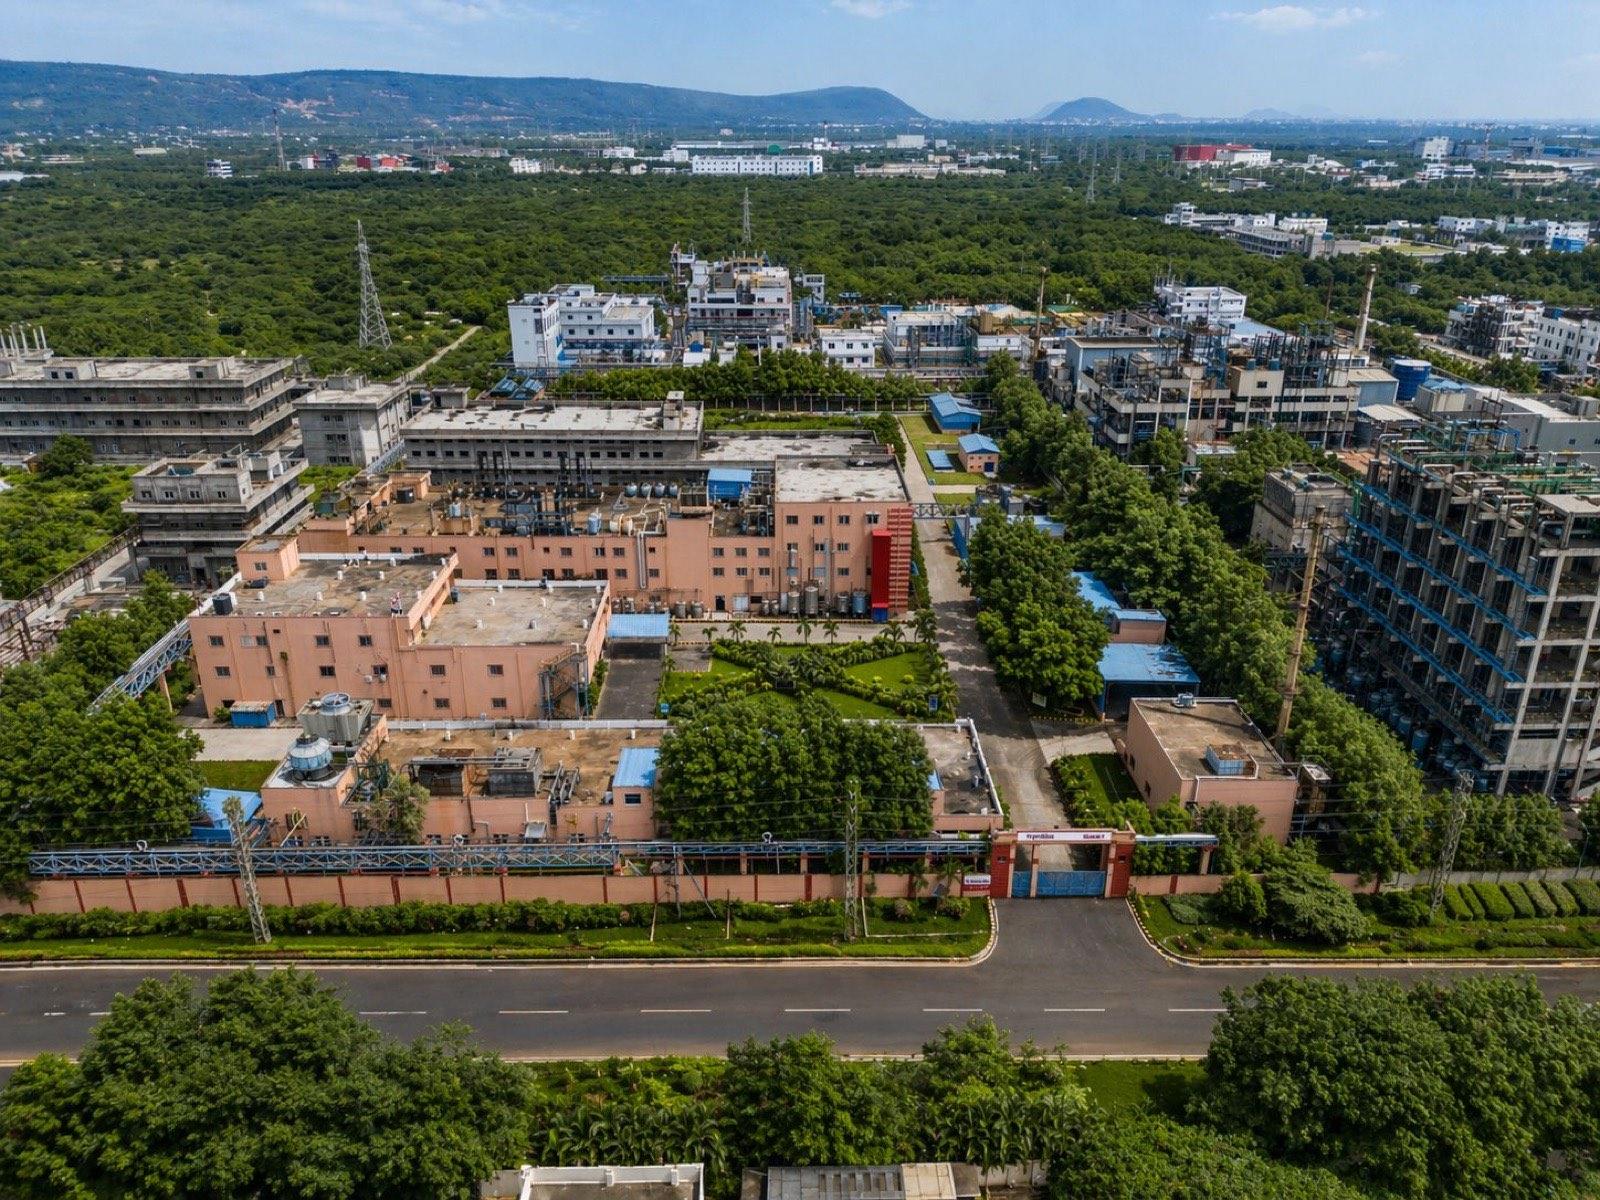
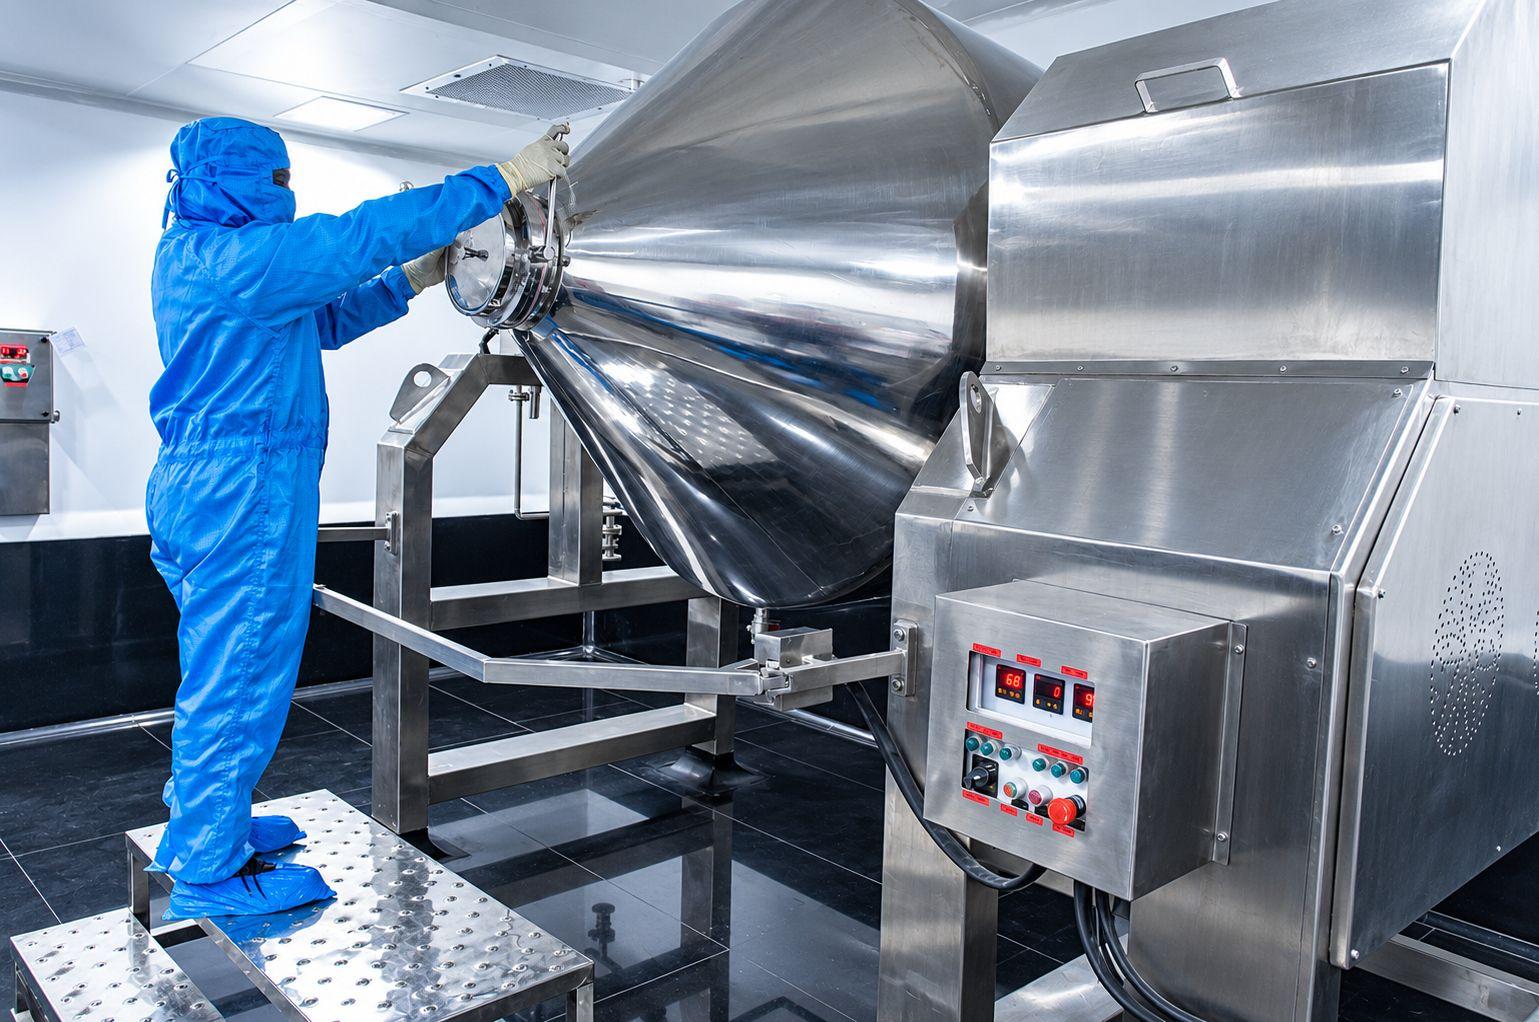
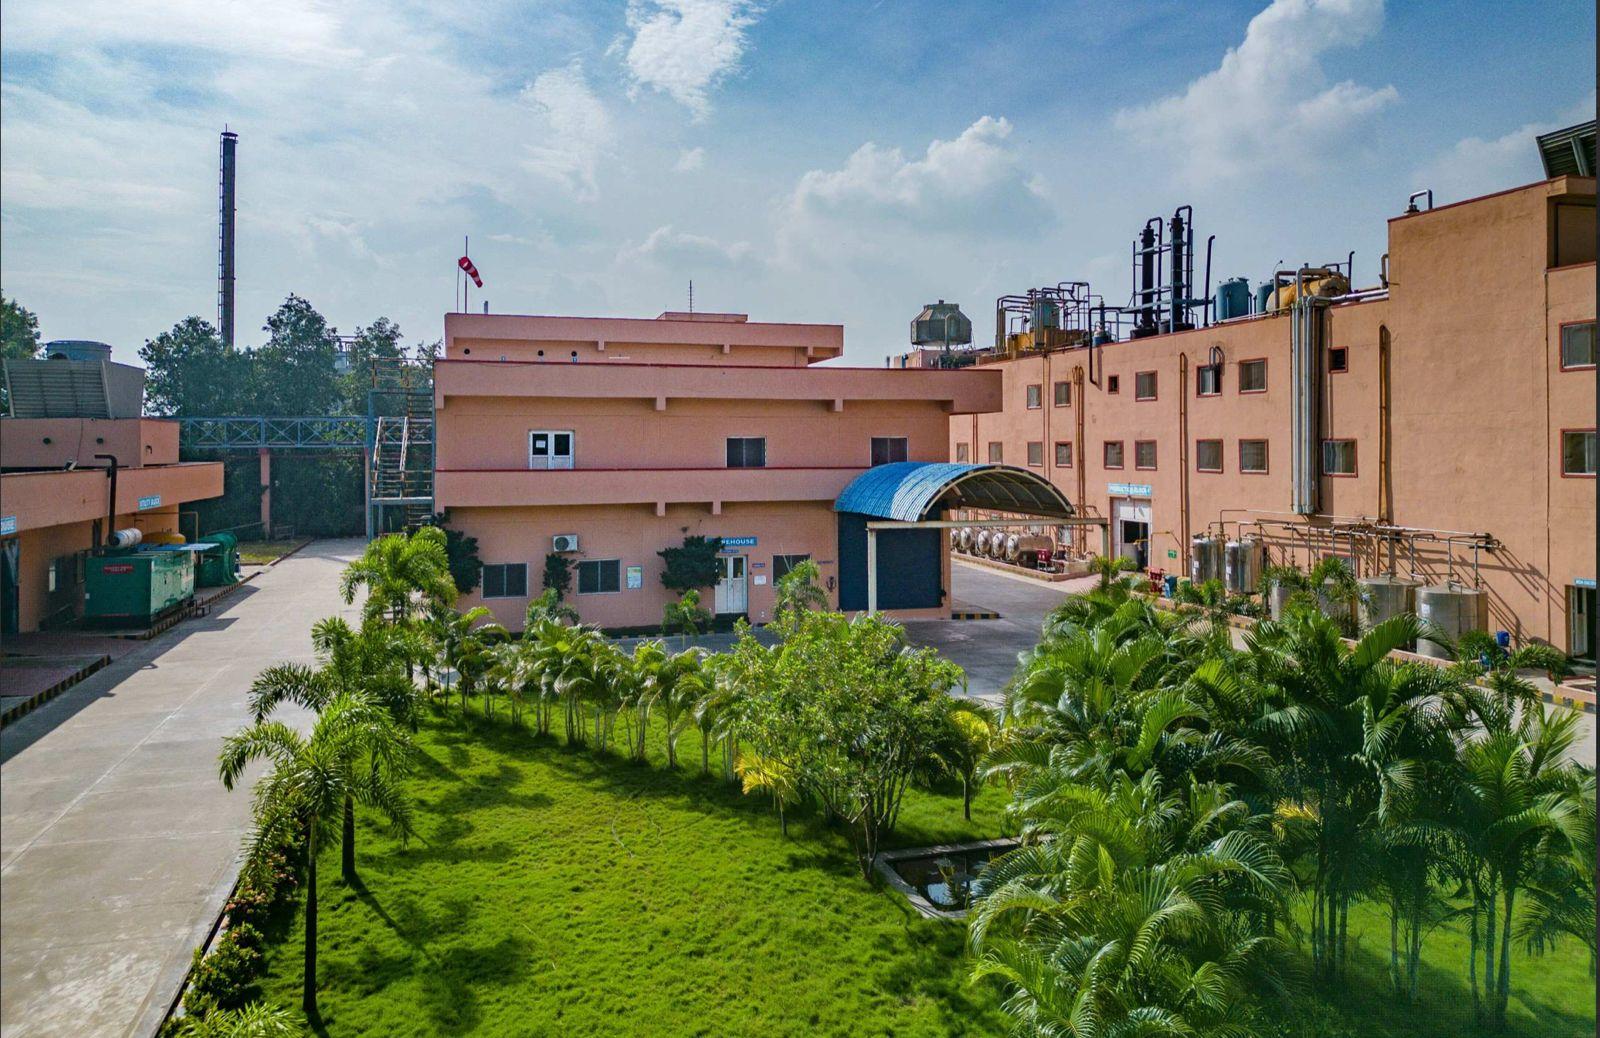
Our Vizag Facility is the flagship of Symbio's API manufacturing network, built to support technically demanding API and intermediate programmes from specialised, smaller-volume campaigns through sustained commercial manufacturing.
The site combines flexible manufacturing, broad synthesis capability and an expanding regulated-market platform, with significant capacity expansion underway.
The site supports both small-volume, high-value programmes and larger commercial campaigns, with batch capability ranging from approximately 2 to 10 kg on specialised lines to 100 to 300 kg on high-volume lines. Around 35 stainless-steel and glass-lined reactors, ranging from 100 L to 8 KL, support this flexibility.
Technical capability
- Multi-step API and intermediate synthesis
- Small-volume and commercial-scale manufacturing
- Stainless-steel and glass-lined processing from 100 L to 8 KL
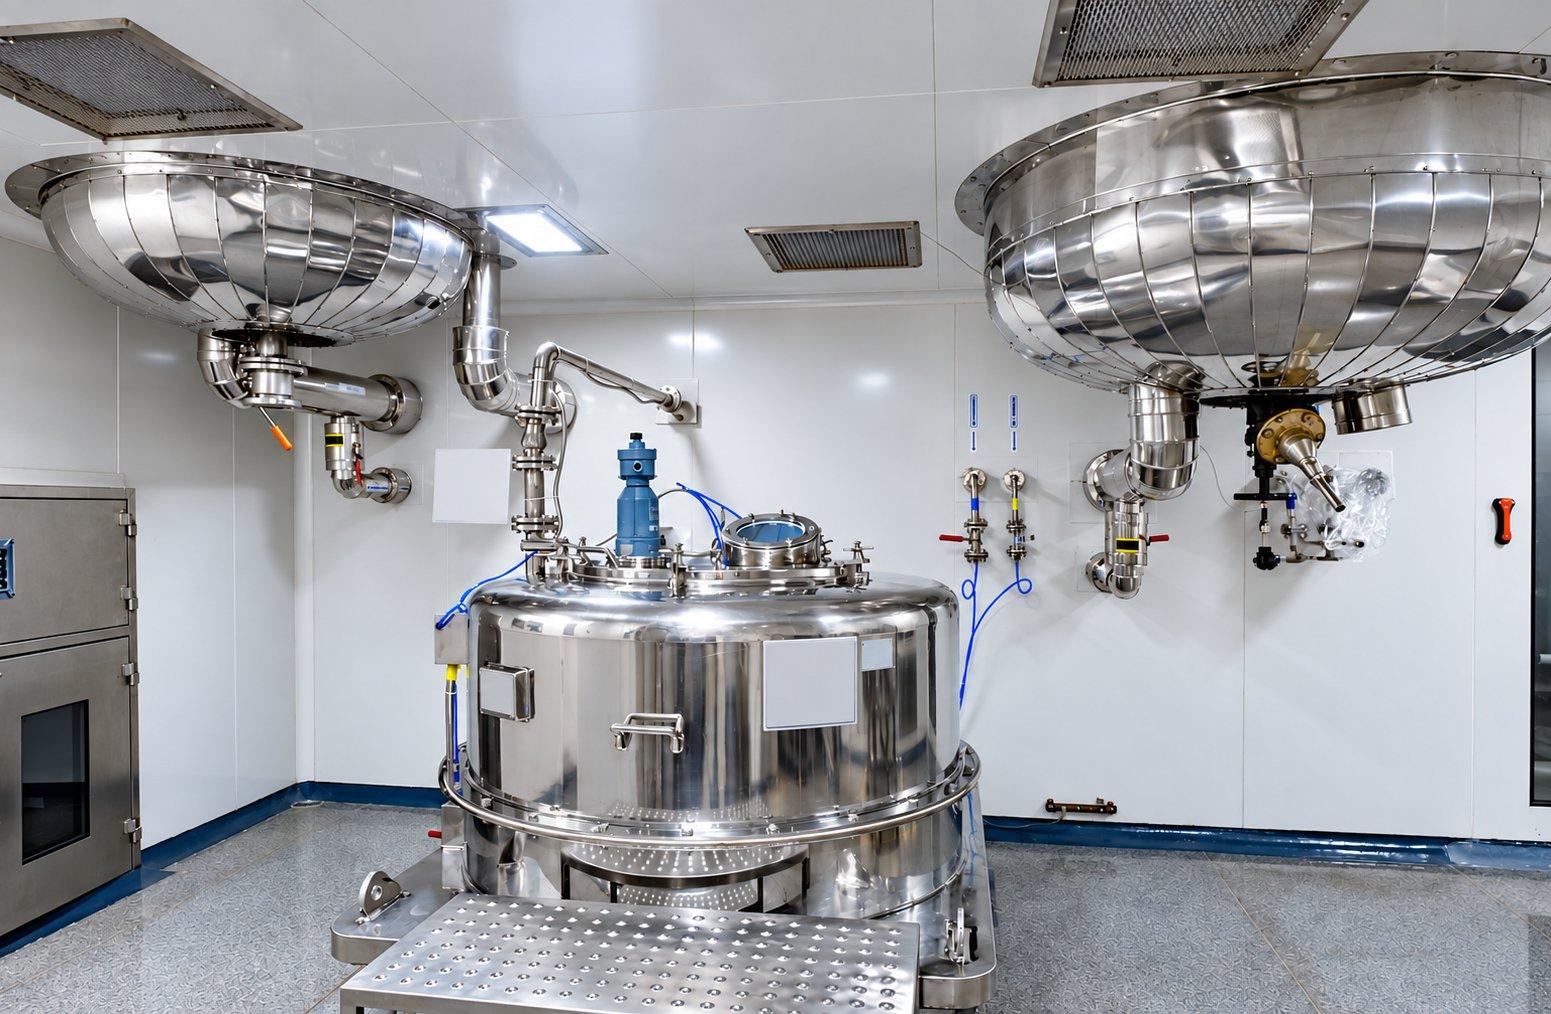
- Multiple isolation and drying configurations
- Particle-size reduction capability
- Internal technology transfer from central R&D into GMP manufacturing
- Peptide and specialised synthesis capability under development
Regulatory & global-market platform
- WHO-GMP manufacturing
- CEP-approved products already in place
- Selected products supported by US DMFs and EU ASMFs
- ANVISA registration underway
- Customer programmes supporting the US and other regulated-market pathways
API + dedicated pre-formulation
VPL Facility
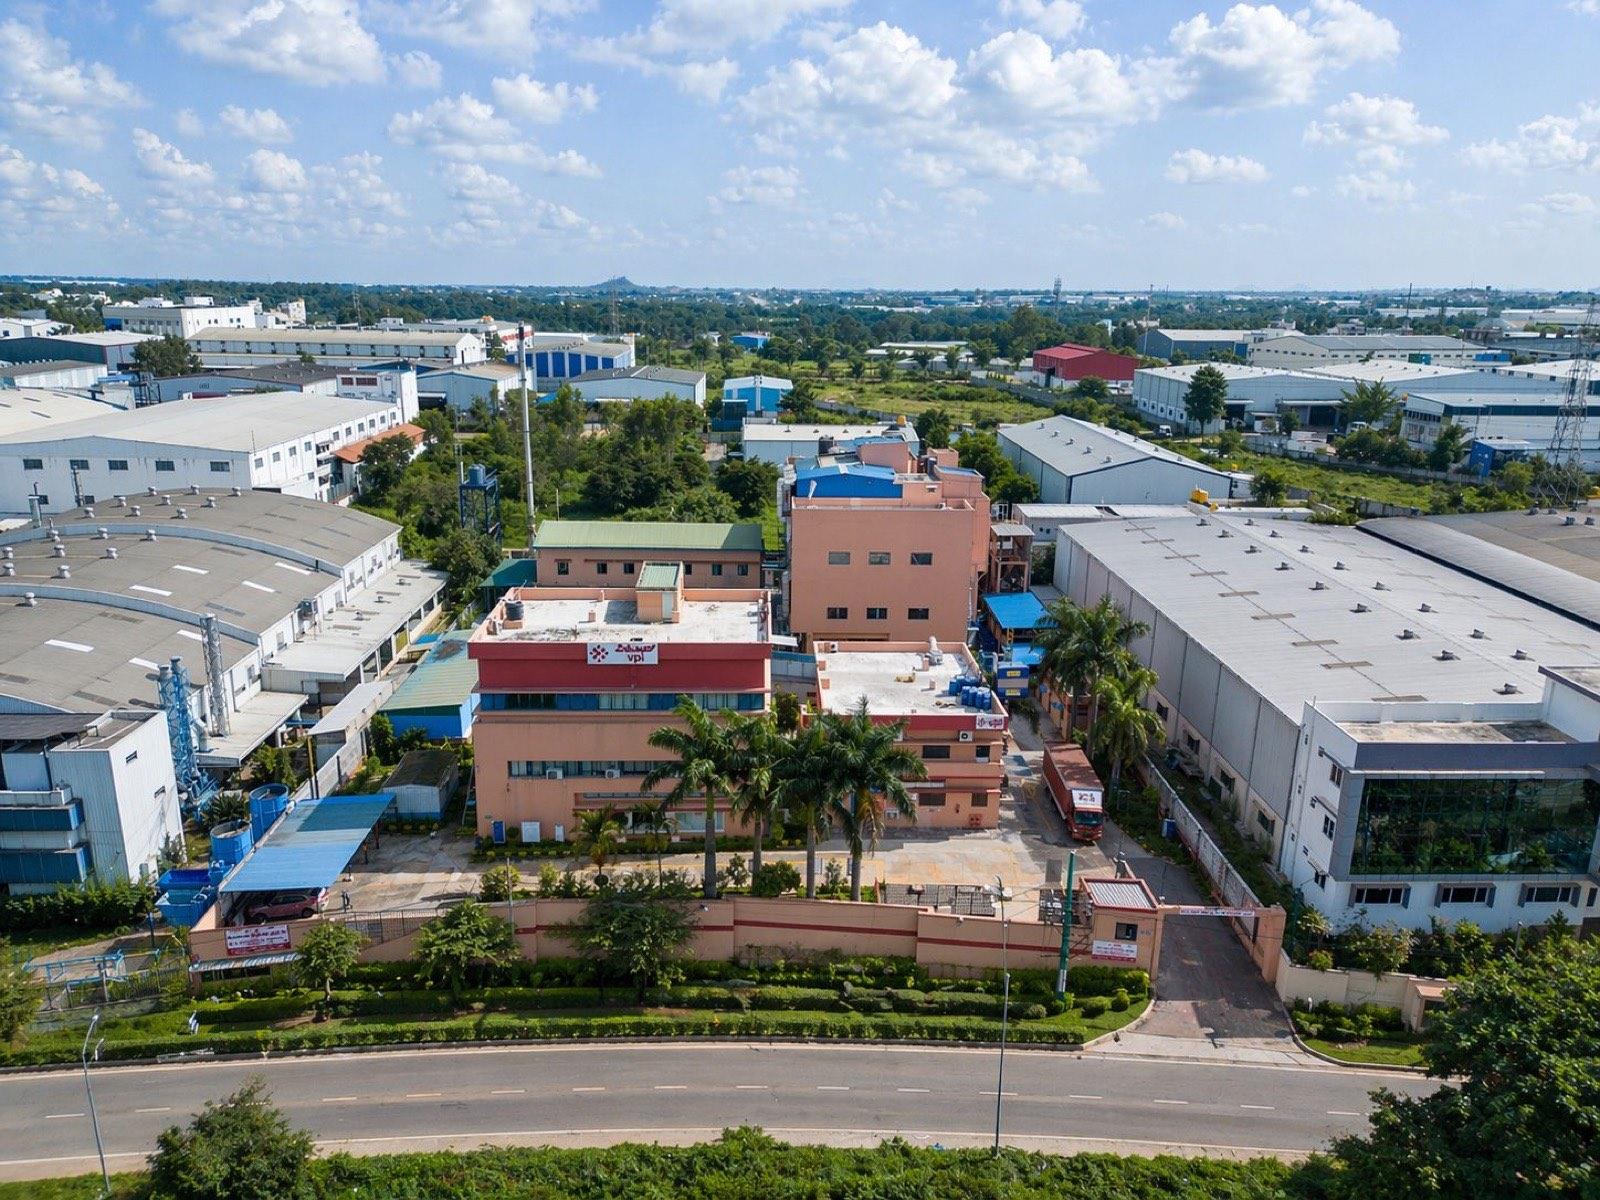
Focused API and regulated-market pre-formulation capability.
3
Dedicated GMP production modules
1
Dedicated pellets & granules line
2026
EDQM Certified
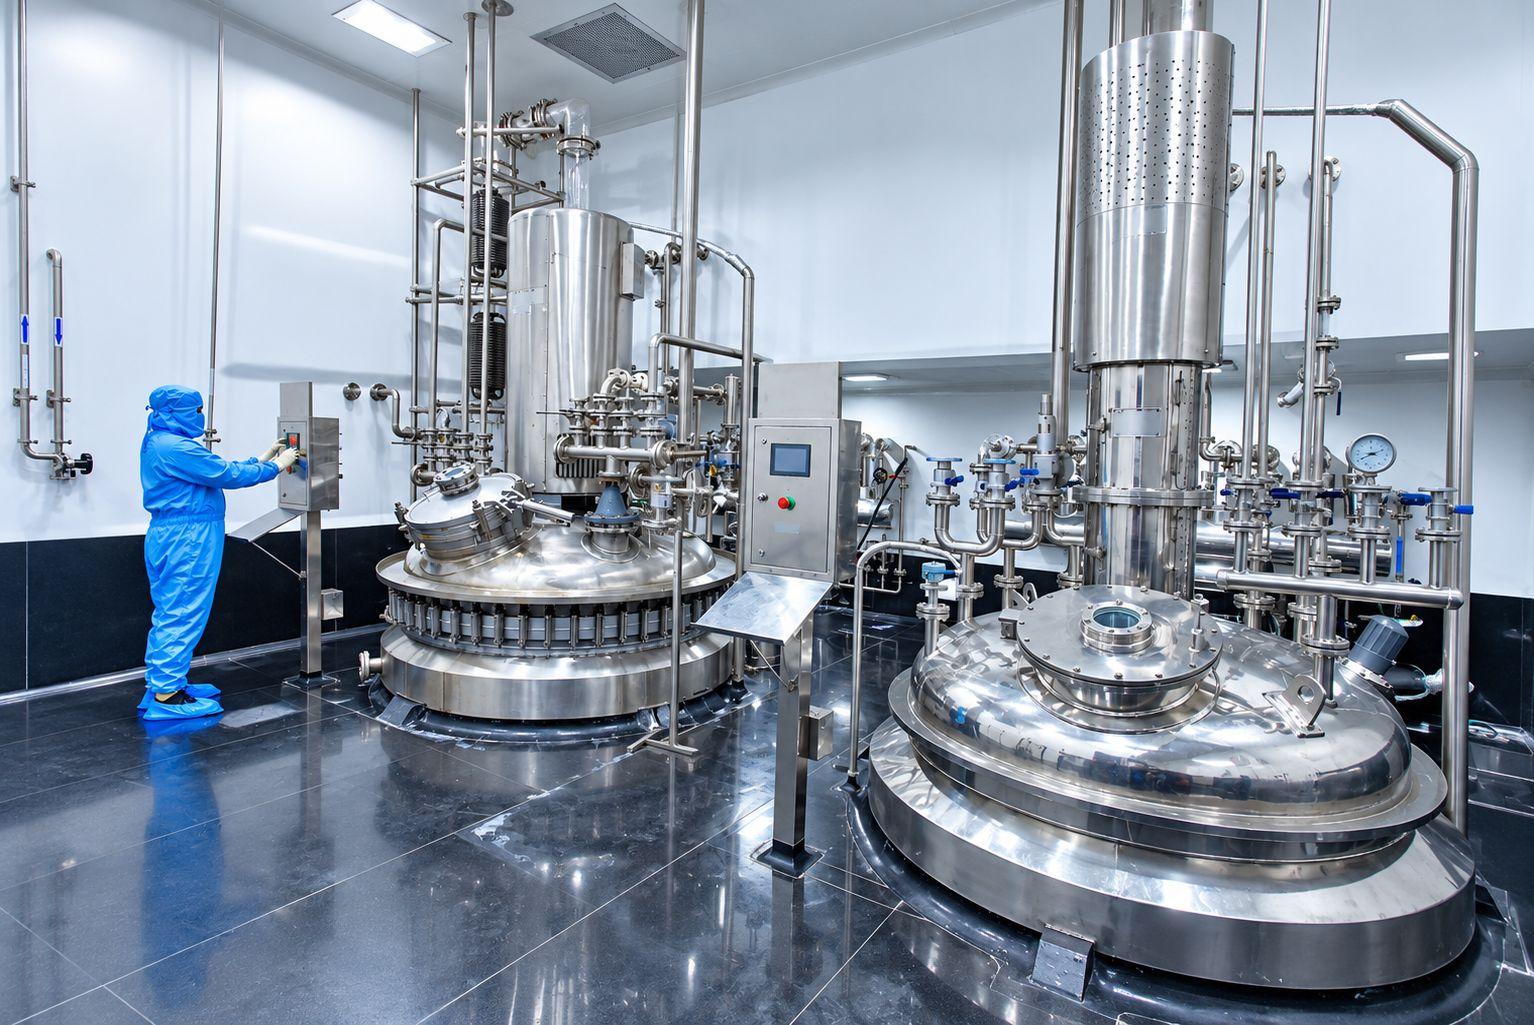
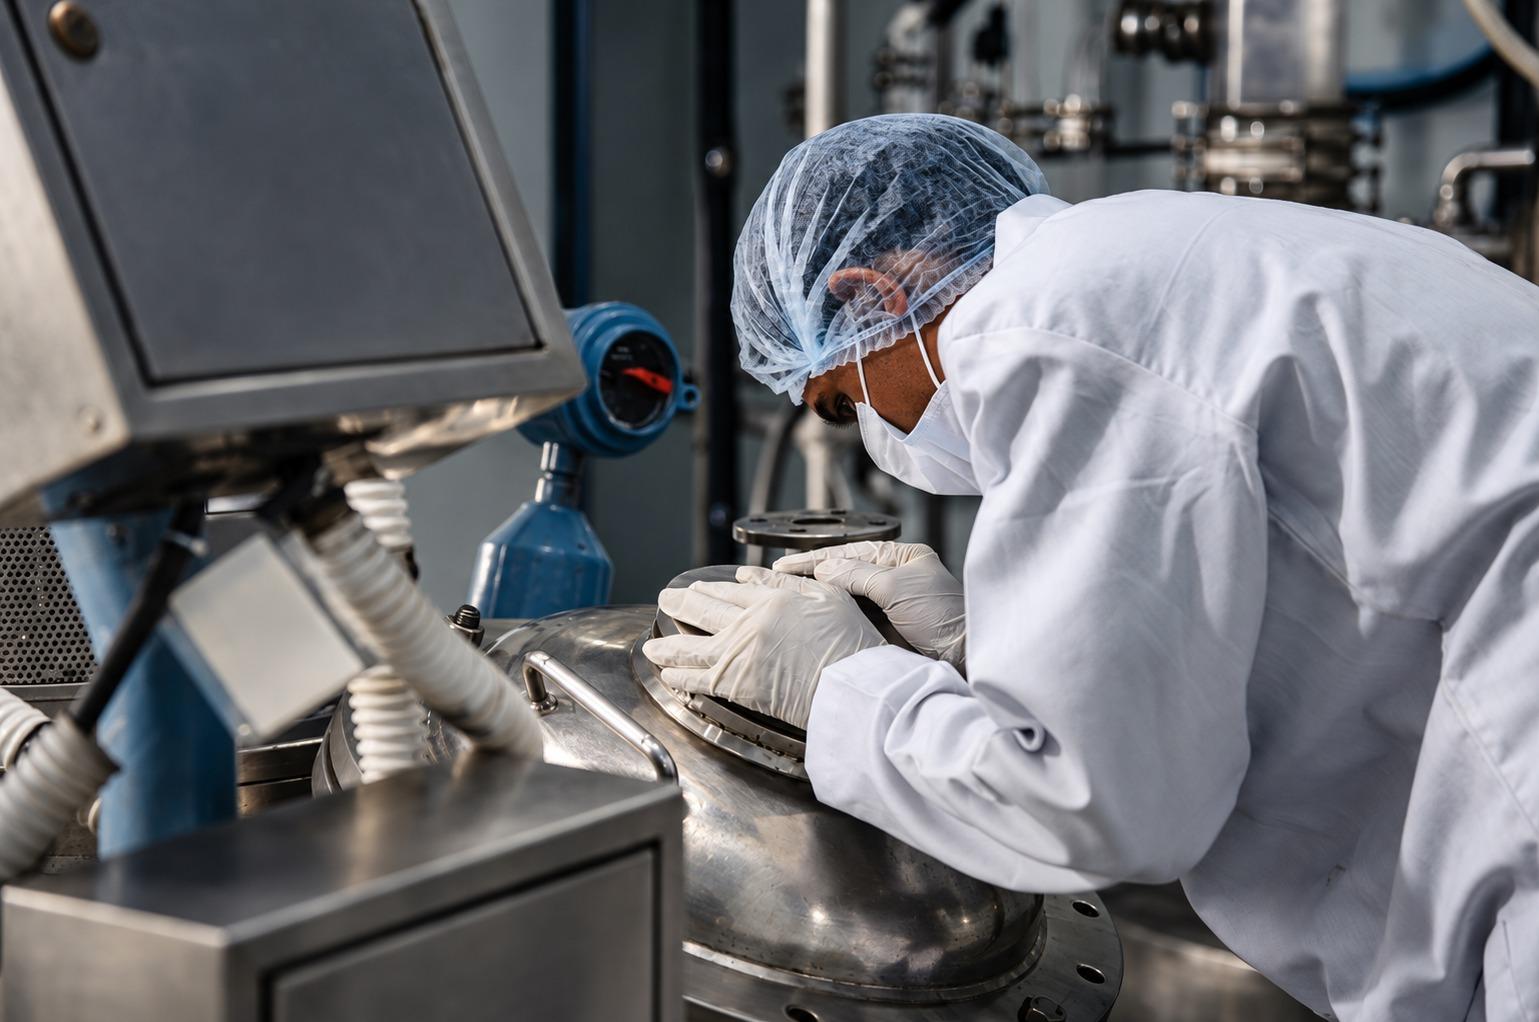
The VPL Facility combines focused API manufacturing with a distinct, dedicated pellets & granules platform.
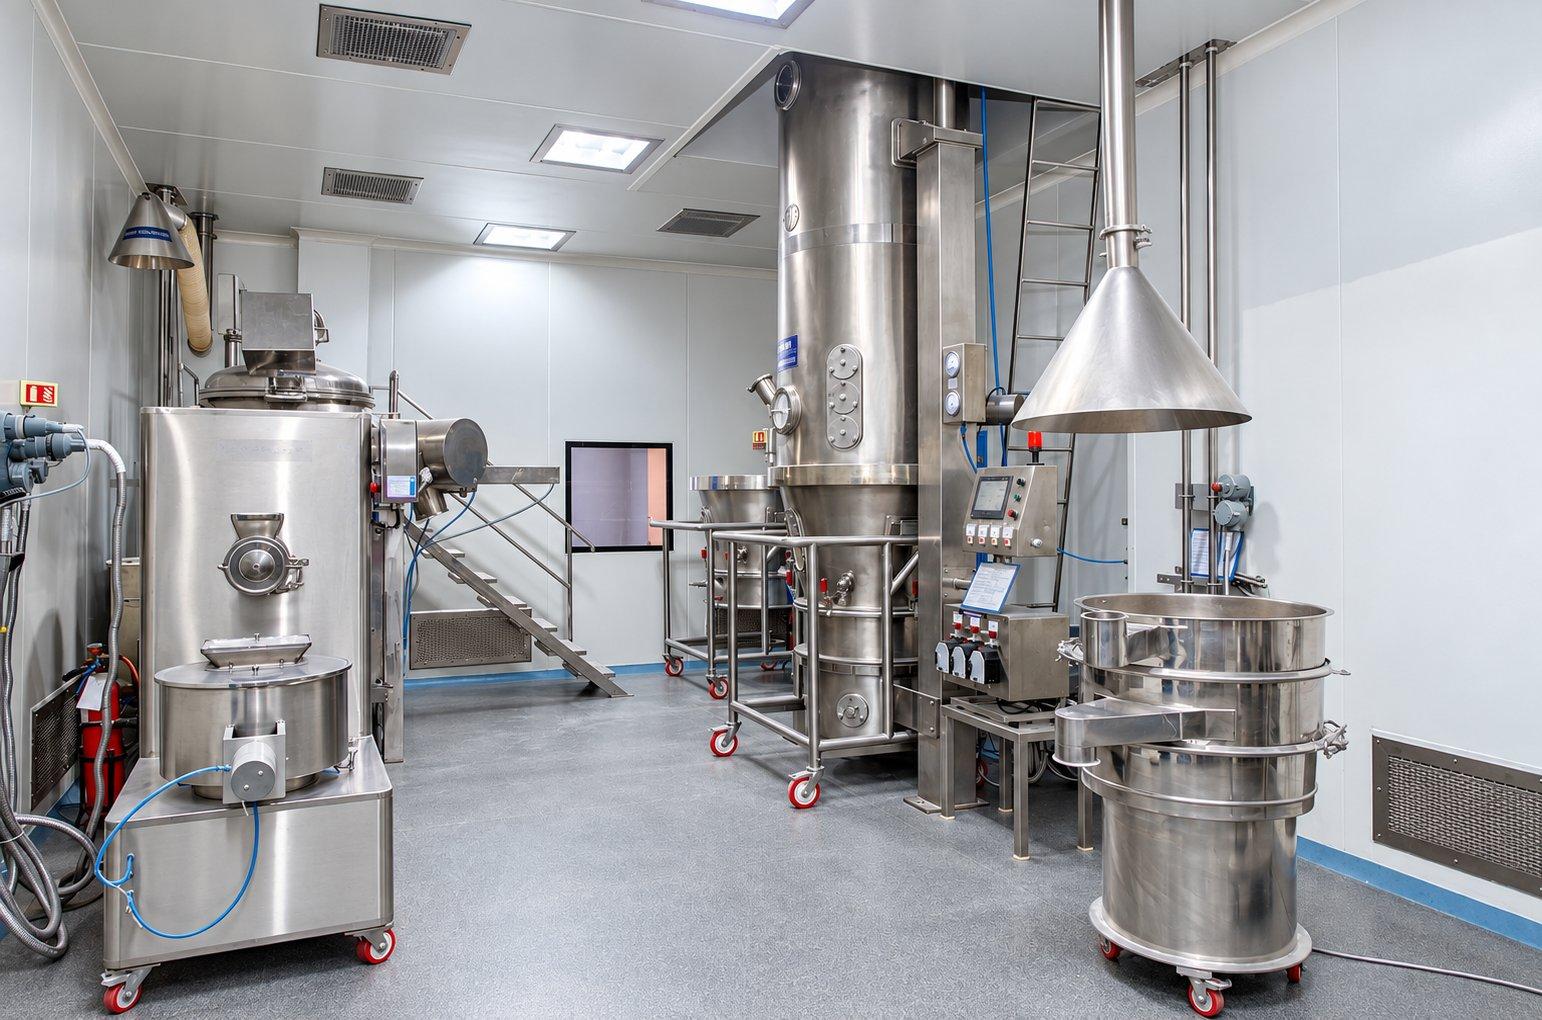
Its pre-formulation capability is built around extrusion-spheronization, supported by rapid mixer granulation, fluid-bed processing and dedicated pellet-manufacturing infrastructure, with formulation R&D supporting development alongside manufacturing.
Importantly, this platform is being developed with global regulated-market requirements in mind, including the US and Europe. The objective is not simply to offer pellets & granules as another manufacturing service, but to build a technically robust pre-formulation platform capable of supporting customer programmes from development through commercial manufacturing.
Pre-formulation capability
- Multi-suite product development
- Skilled R&D, production and analytical manpower
- Expertise in handling proteolytic enzymes
- Formulation R&D and optimisation support
- Customer-led pre-formulation development
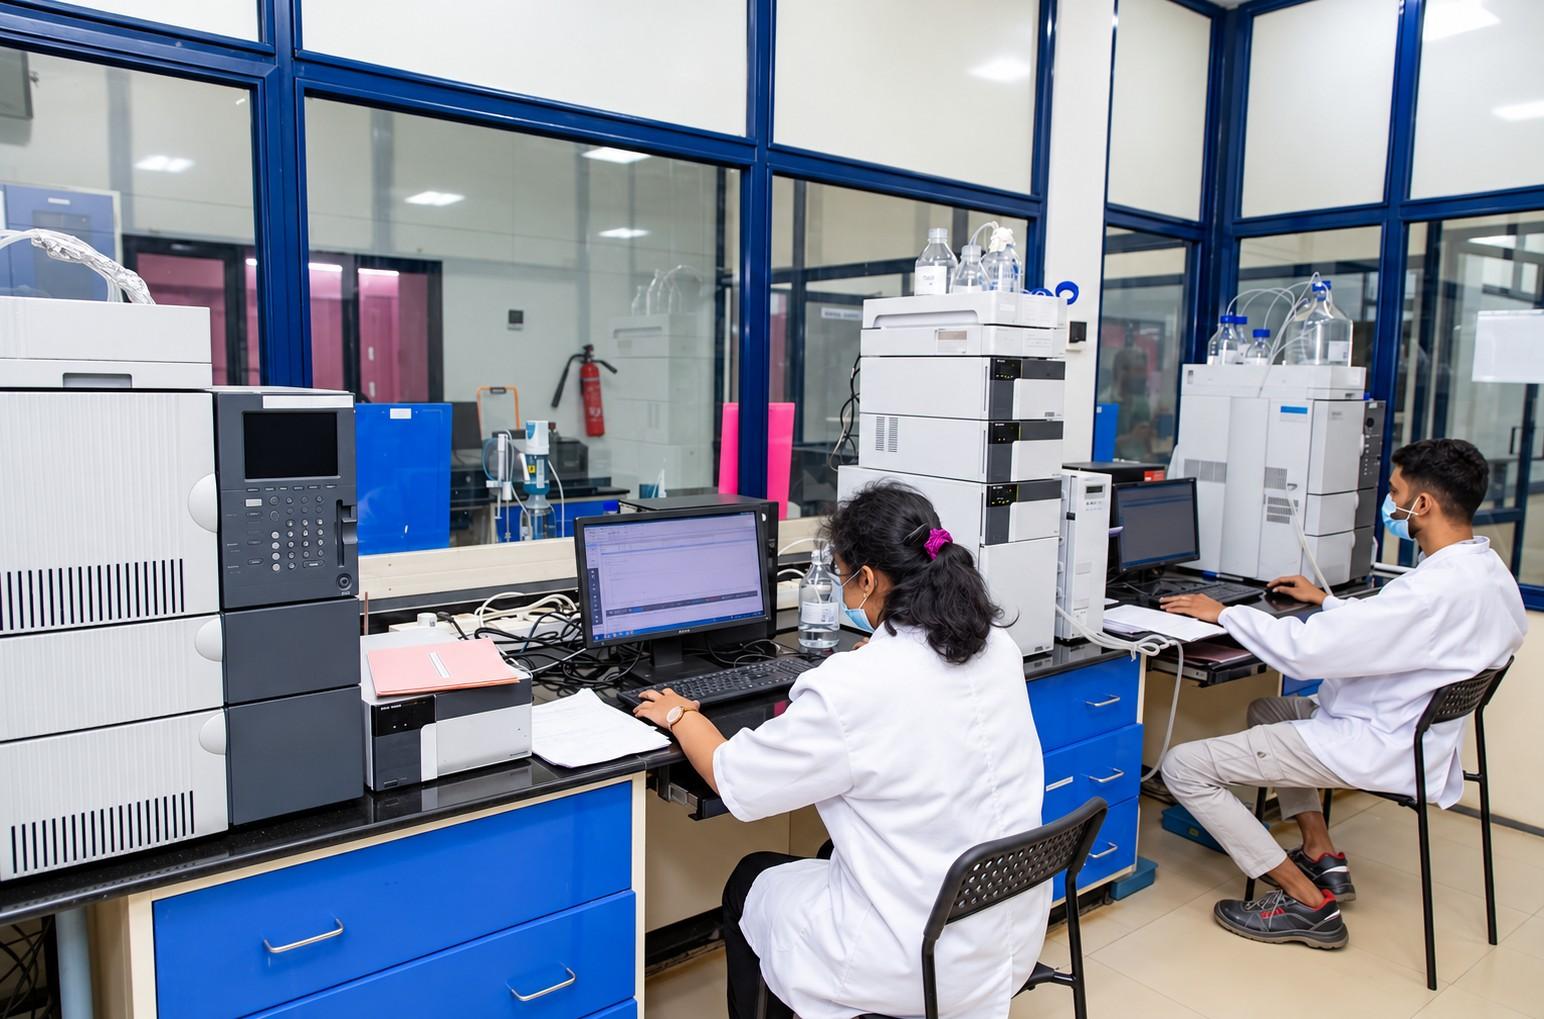
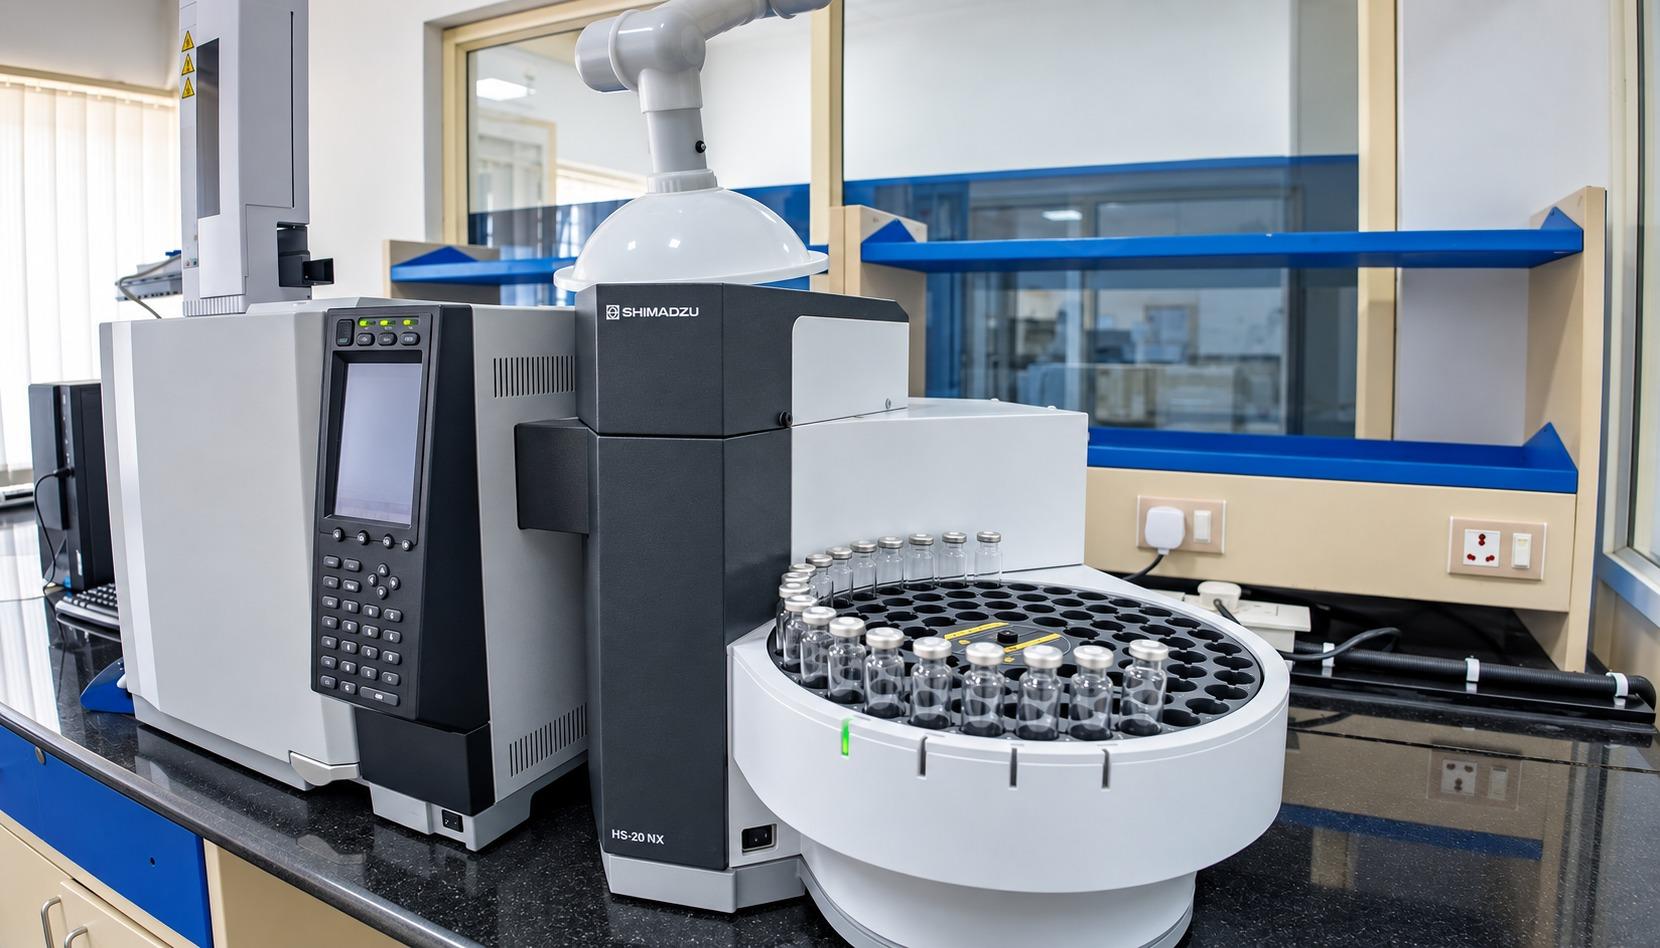
- Integrated analytical support for product development and evaluation
API & regulatory platform
- Focused API manufacturing
- ANVISA-approved operations
- CEP-linked products
- EDQM Certified in 2026
- International supply across regulated and emerging markets
Enzymes + Specialised Synthesis
Tumkur Facility
Pharmaceutical enzymes, specialised synthesis and hydrogenation.
2
Production blocks
100 L – 8 KL
Reactor capability
High-pressure
Catalytic hydrogenation
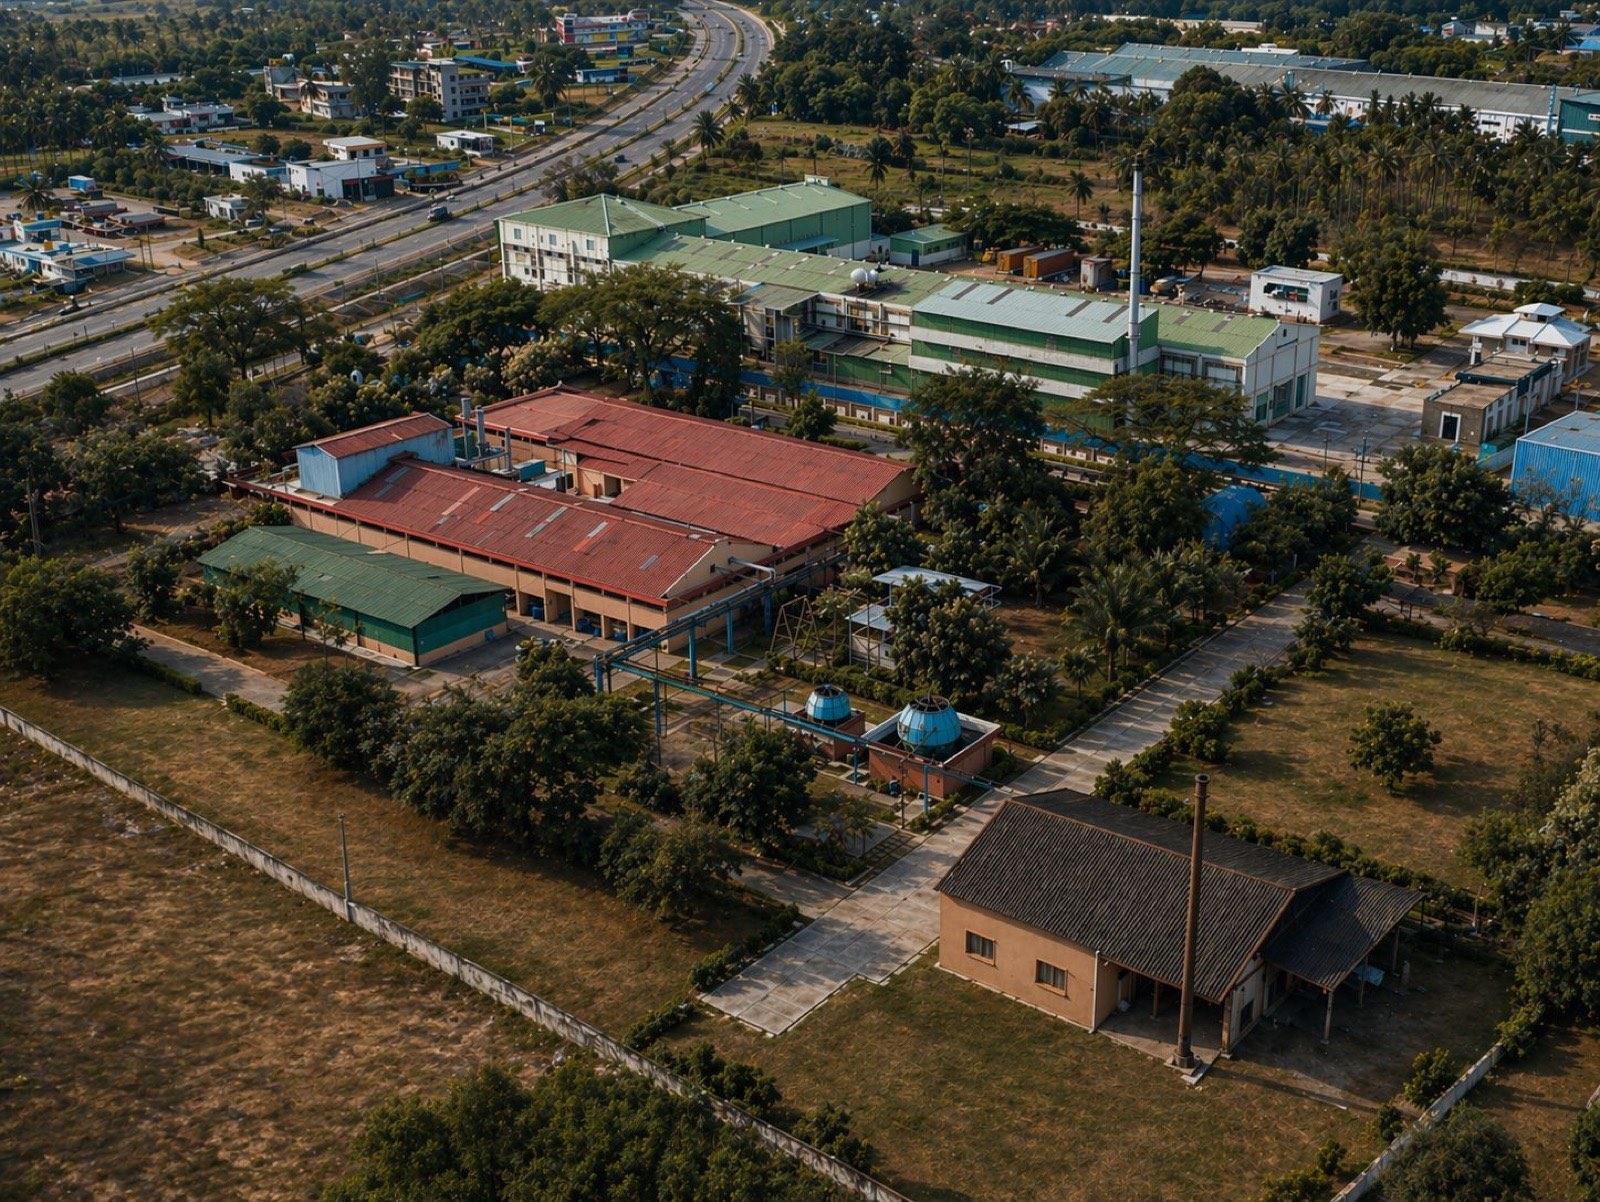
The Tumkur Facility combines pharmaceutical-enzyme and bulk API manufacturing with dedicated capability for specialised synthesis and high-pressure catalytic hydrogenation.
Two production blocks provide flexibility across larger-volume enzyme and API programmes as well as more specialised synthesis campaigns, with reactor capability extending from approximately 100 L to 8 KL.
The site retains meaningful room for future expansion within the existing campus, with utility infrastructure already in place to support additional manufacturing capability over time.
Technical capability
- Dedicated pharmaceutical-enzyme manufacturing
- Bulk API and intermediate synthesis
- Dedicated specialised-synthesis capability
- High-pressure catalytic hydrogenation
- Stainless-steel and glass-lined processing
- Reactor capability from 100 L to 8 KL
- Multiple isolation and drying technologies
- Campaign-based manufacturing